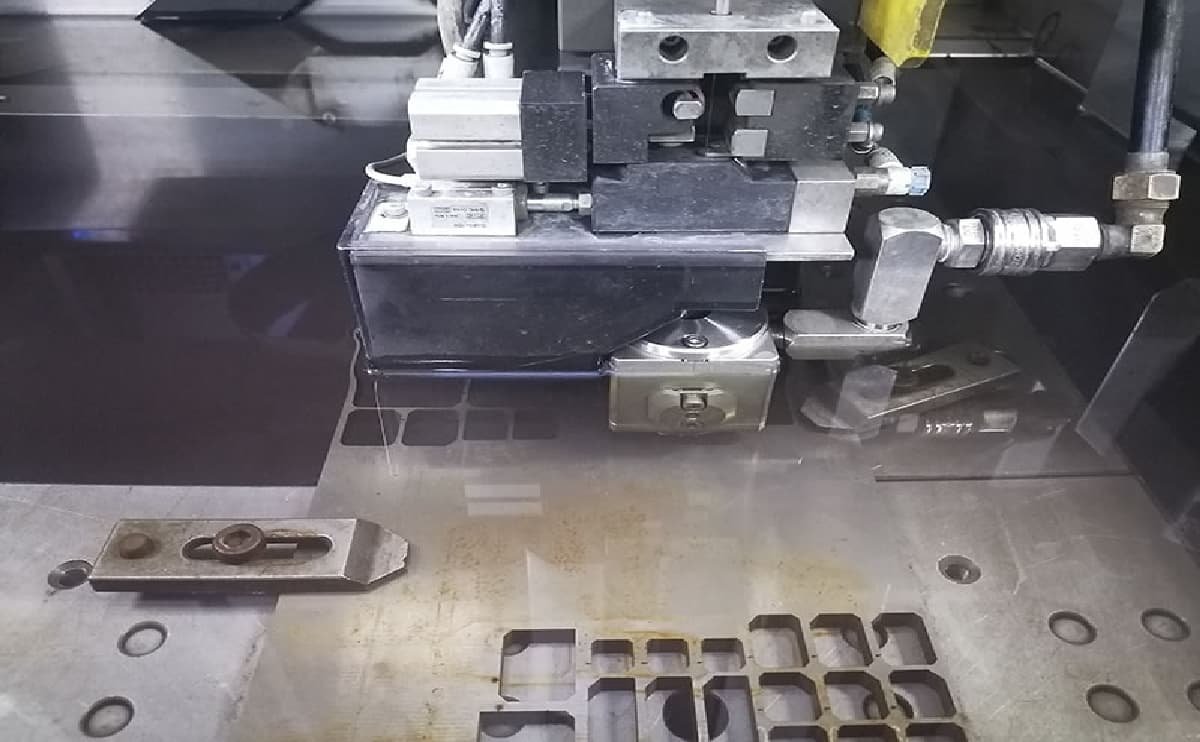
Slow Wire Cutting
Slow wire cutting , also known as Wire-cut EDM (Electrical Discharge Machining) , is a non-contact material removal process. A discharge gap of a few microns is maintained between the wire electrode and the workpiece, and the metal is melted or vaporized by the intense, instantaneous heat (8,000–12,000°C) generated by electrical discharges.
Because the process relies on electrical erosion, it is unaffected by the hardness of the material.
There is no need for custom-made cutting tools; the process can directly produce sharp corners, narrow slots, complex-shaped holes, tapered features, and intricate 3D profiles with varying top and bottom geometries. The kerf (cut width) is only 0.02–0.05 mm larger than the wire diameter, the minimum internal corner radius (R) can reach 0.02 mm, and micro-holes as small as φ0.03–0.05 mm can be machined.
The absence of mechanical cutting forces makes it exceptionally well-suited for thin-walled components (<0.5 mm) and micro-structures, resulting in surfaces free from micro-cracks and virtually devoid of burrs.
Through multiple passes—including roughing, semi-finishing, finishing, and ultra-finishing—dimensional accuracy can be refined to the ±1 μm level, and surface roughness (Ra) can reach a mirror-like finish, eliminating the need for subsequent polishing or grinding operations.
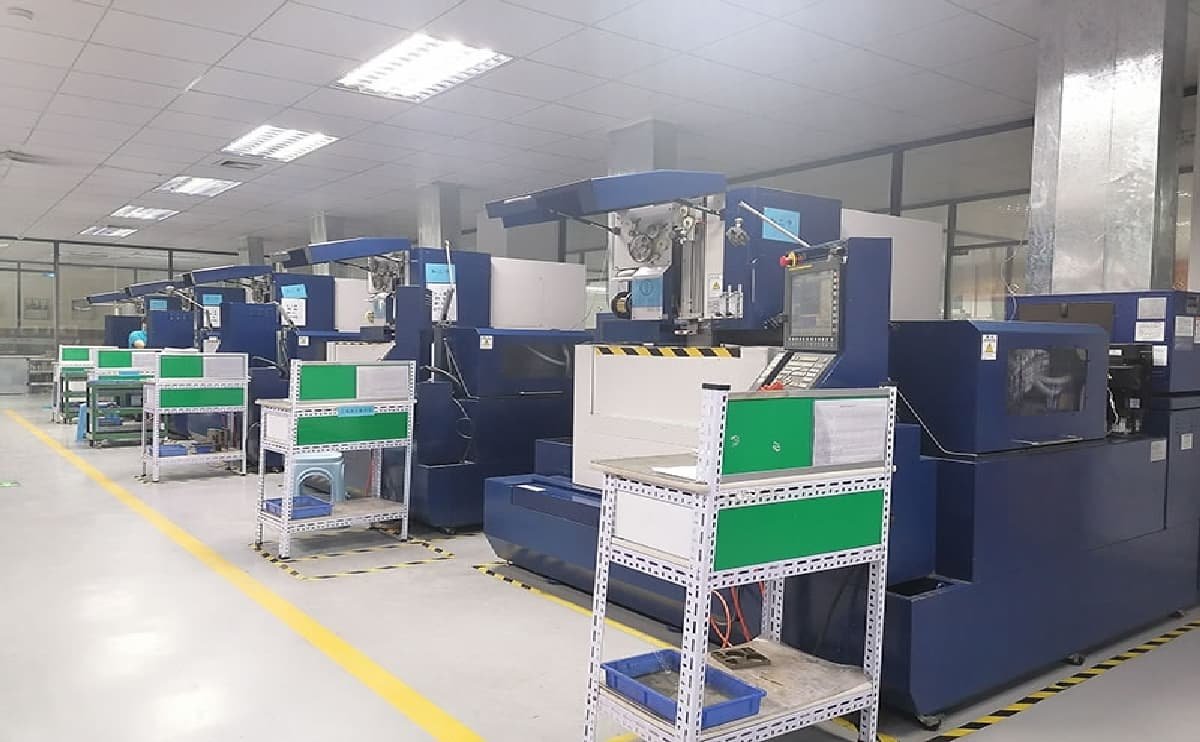
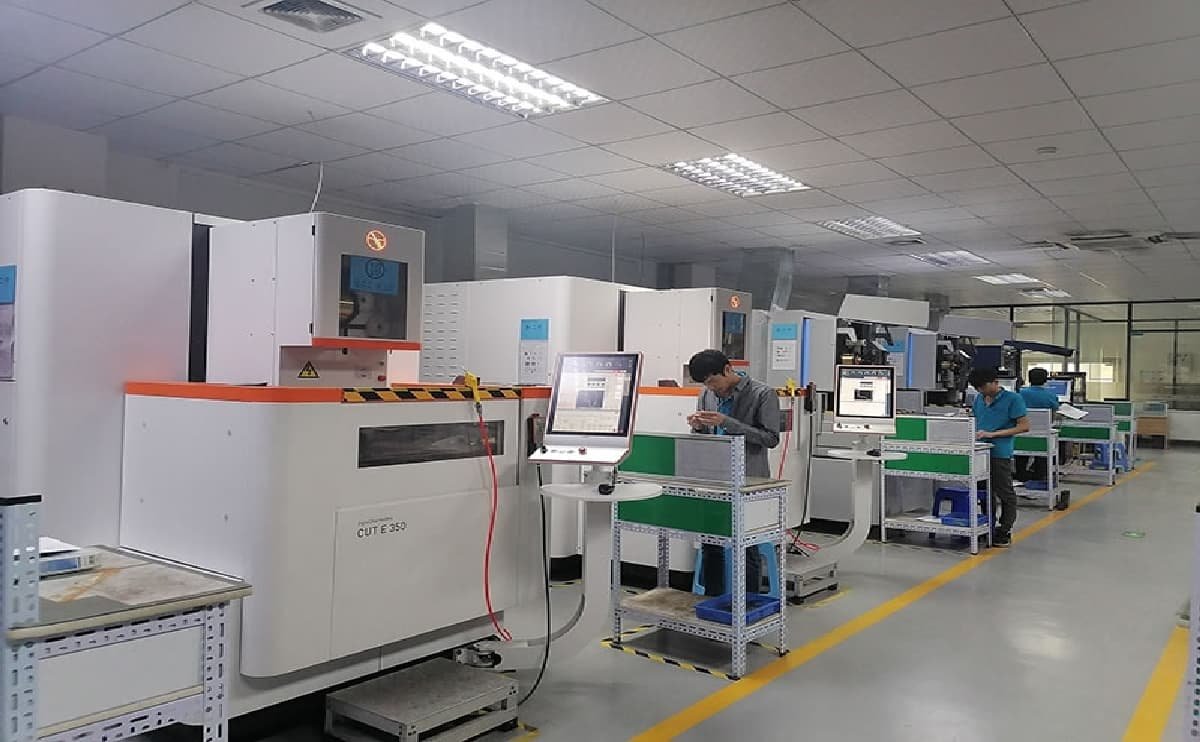
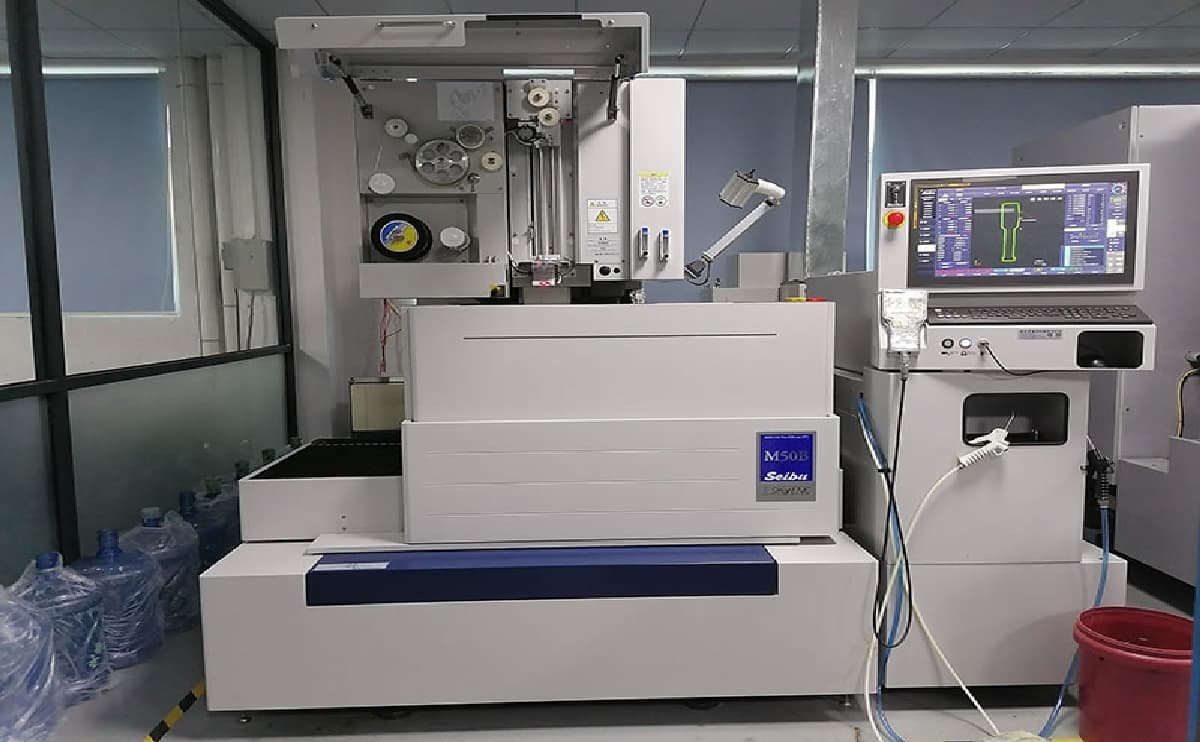
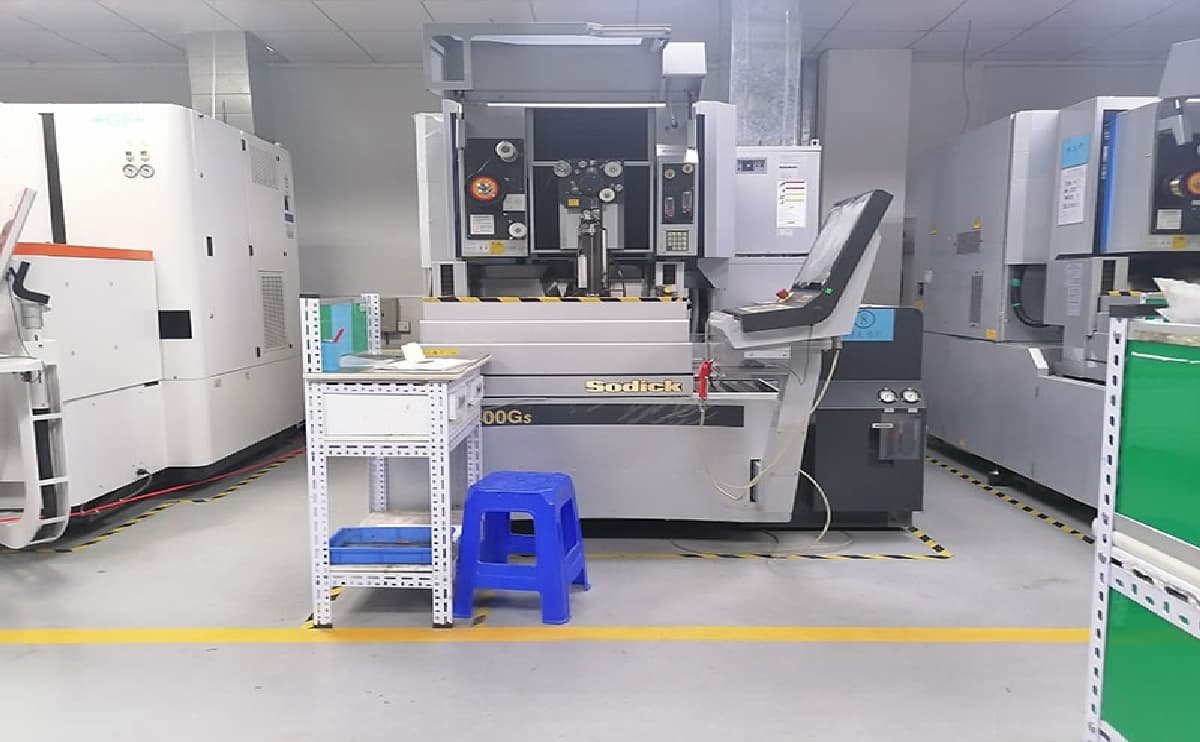
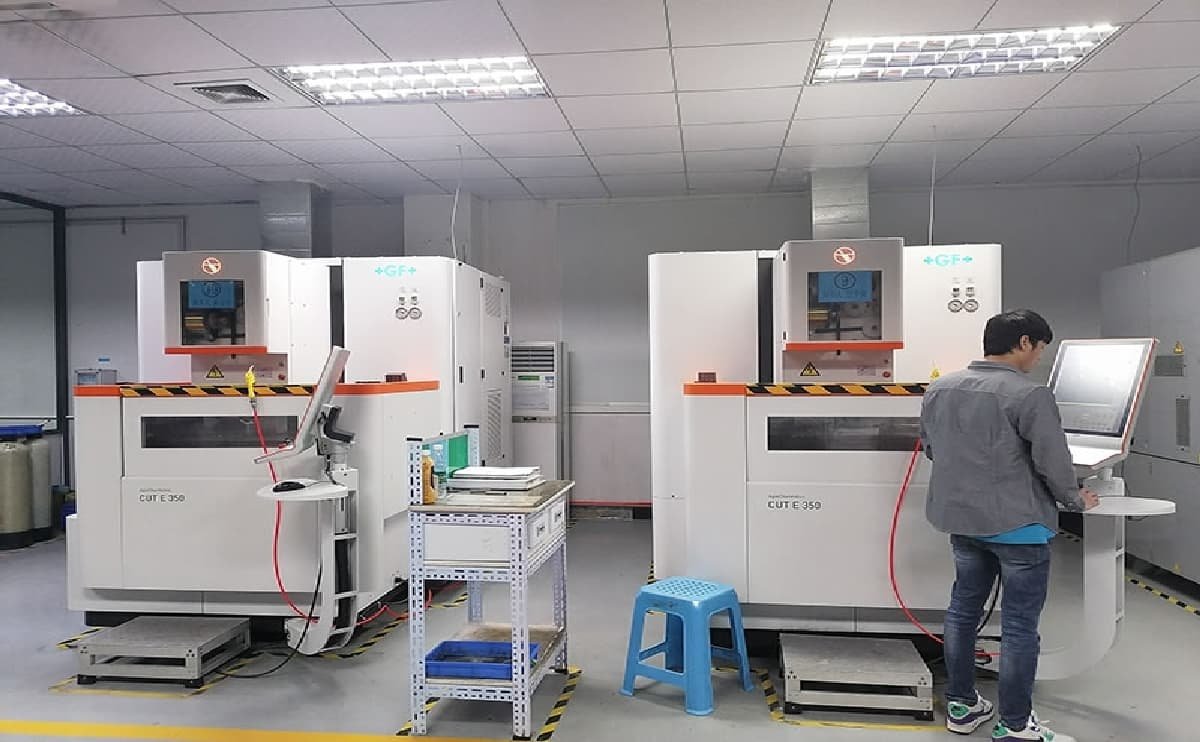
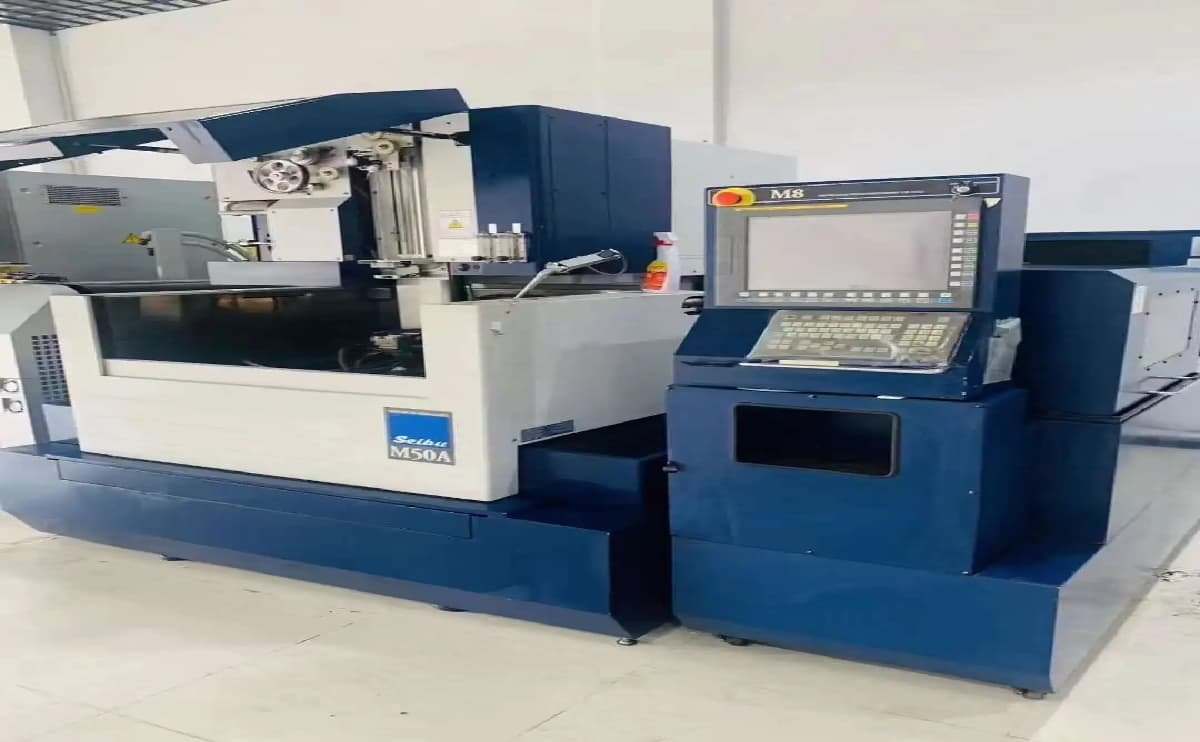
Our typical machining equipment: